Carbon Steel A350 LF2 Round Bar
Carbon Steel A350 LF2 Round Bar manufacturer & supplier. Impact-tested forging grade specified for low-temperature piping service. Ask for a fast quote.
Round Bars Wholesaler, Exporter & Supplier
Carbon steel round bars are solid cylindrical steel products used for structural frameworks, machined components, shafts, pins and other industrial parts. But a grade and diameter alone don’t always define the complete product: a purchase may also need a product standard, length, manufacturing route, tolerance, surface finish, material condition, testing and documentation. EN 10083-2 and EN 10025-2, for example, govern engineering and structural carbon steel bars respectively, covering everything from general construction to quenched and tempered machine parts.
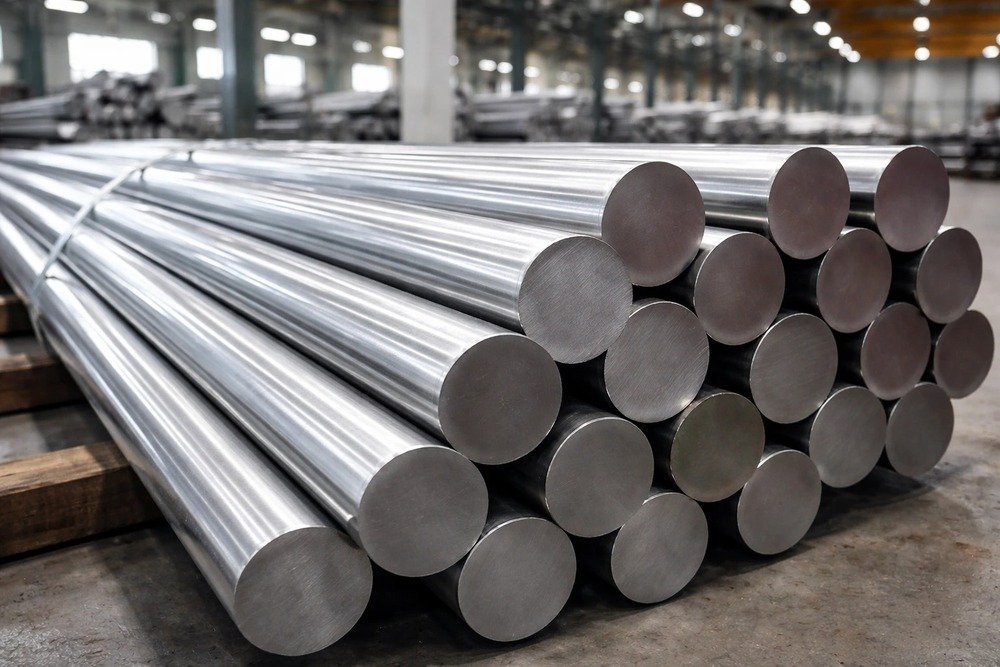
Carbon Steel A350 LF2 Round Bar manufacturer & supplier. Impact-tested forging grade specified for low-temperature piping service. Ask for a fast quote.
Carbon Steel A105 Round Bar manufacturer & supplier. The forging grade widely machined into flanges, fittings and valve parts. Enquire for stock and price.
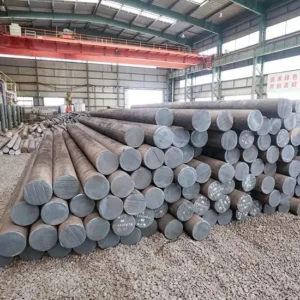
Buy Carbon Steel S235JR Round Bar from a trusted manufacturer & supplier. EN 10025-2 bar, 235 MPa yield, 27 J at +20 degC. Competitive prices, fast quote.
Buy Carbon Steel S420 Round Bar from a trusted manufacturer & supplier. EN 10025-3 bar, 420 MPa yield, 40 J at -20 degC. Competitive prices and fast quotation.
Buy Carbon Steel A694 F52 Round Bar from a trusted manufacturer & supplier. ASTM A694 forging bar, 52 ksi yield, 71 ksi tensile. Competitive prices, fast quote.
Buy Carbon Steel A694 F60 Round Bar from a trusted manufacturer & supplier. ASTM A694 forging bar, 60 ksi yield, 75 ksi tensile. Competitive prices, fast quote.
Buy Carbon Steel A694 F65 Round Bar from a trusted manufacturer & supplier. ASTM A694 forging bar, 65 ksi yield, 80 ksi tensile. Competitive prices, fast quote.
Buy Carbon Steel A694 F70 Round Bar from a trusted manufacturer & supplier. ASTM A694 forging bar, 70 ksi yield, 85 ksi tensile. Competitive prices, fast quote.
Buy Carbon Steel C45 Round Bar from a trusted manufacturer & supplier. EN 10083-2 bar, 490 MPa +QT yield, 6-250 mm, cut to size. Competitive prices, fast quote.
Buy Carbon Steel S275JR Round Bar from a trusted manufacturer & supplier. EN 10025-2 bar, 275 MPa yield, 27 J at +20 degC. Competitive prices, fast quote.
Buy Carbon Steel S355JR Round Bar from a trusted manufacturer & supplier. EN 10025-2 bar, 355 MPa yield, 27 J at +20 degC. Competitive prices, fast quote.
Buy Carbon Steel S355J2 Round Bar from a trusted manufacturer & supplier. EN 10025-2 bar, 355 MPa yield, 27 J at -20 degC. Competitive prices, fast quote.
A carbon steel round bar is a solid cylindrical steel product supplied to defined material, dimensional, condition and quality requirements. It helps to think about a purchase like this in five stages: first the service requirement the part has to survive, then the material and governing standard that satisfy it, then the production route used to make it, then the exact geometry and condition needed, and finally the testing and documentation that prove all of that was actually delivered.
A carbon steel round bar is a solid cylindrical carbon-steel product, and its complete specification can include its grade, product standard, diameter, length, manufacturing route, tolerance, surface finish, material condition and required documentation. The product specification, in practice, is the complete set of technical and commercial requirements that determines what a supplier is expected to deliver.
Nine things typically define the product. The grade establishes the material identity and carbon content. The product standard identifies the governing specification. Diameter sets the intended cross-sectional size, and length determines how the bar is prepared and handled. The manufacturing route can affect dimensional and surface characteristics. Tolerance defines the acceptable dimensional deviation. Surface finish affects machining and downstream use. Material condition (like normalized or quenched and tempered) dictates the mechanical properties. And testing or documentation supports conformity and acceptance.
Consider a request for a C45 carbon steel round bar, 50 mm. That identifies the grade and nominal diameter, but it doesn’t tell the supplier which product standard governs, what length is required, what tolerance is acceptable, what surface finish is needed, what heat-treatment condition is required, or what certification and testing is expected.
Before sending an enquiry, define the application, record the required grade, identify the product standard, note diameter and length, define any critical tolerance or finish, state the required testing and documentation, and confirm quantity and destination.
The most common mistake is treating grade plus diameter as a complete specification. Important supply requirements get left undefined that way, so it helps to complete the relevant fields rather than assume a 50 mm bar from one supplier matches a 50 mm bar from another (tolerance and metallurgical condition can differ significantly). It also helps to resist copying a supplier’s entire specification table into an RFQ. Not every field they list will be relevant to your part, so specify only what actually affects the product you need.
Carbon steel round bars are generally divided into two primary metallurgical and application families: structural steels and engineering steels. They differ fundamentally in how they are designated, what mechanical properties are guaranteed, and how they respond to heat treatment and welding. (BSSA) (worldsteel)
Structural steels are designated by their minimum yield strength and impact toughness. Common grades include S235JR, S275JR, and high-strength variants like S460. They are selected primarily for welding, structural frameworks, and general construction where predictable yield strength and ductility are paramount. Engineering steels are designated by their carbon content and are intended for mechanical engineering, machining, and heat treatment. Common grades include low-carbon options like C20 and C22, medium-carbon workhorses like C30, C35, C45 and C50, and higher-carbon grades like C55 and C60. They are selected for machinability, hardenability, and tensile strength after quenching and tempering.
Additionally, specific forging and high-strength grades exist, such as ASTM A694 F42, which is explicitly designed for high-pressure transmission services and forged fittings.
Within these families, S235JR is the standard baseline structural grade (235 MPa yield). S275JR offers higher yield strengths for heavier loads. C22 (0.17-0.24% C) is often used for low-stress machined parts or case hardening. C35 and C45 are the most widely used medium-carbon grades for general shafts and gears. C50, C55 and C60 are chosen where higher surface hardness and wear resistance are required after heat treatment, offering +QT (quenched and tempered) yields typically ranging from 520 MPa to 580 MPa depending on the diameter.
One assumption is worth being cautious about: the most common grade isn’t automatically the right grade. A familiar grade is only a candidate; the application determines which requirements actually matter. If you know the application but not the grade, the next section walks through a selection method. If you already know the grade but not the exact product form, skip ahead to the standards and specification sections.
Grade selection should start with the conditions the component actually has to withstand, then narrow the candidates by structural load, fabrication method, and mechanical requirements. That’s what a service requirement really is: the environmental, thermal, fabrication and mechanical conditions the component must accommodate.
This approach works best when you know the application but aren’t sure of the grade yet. Start with the primary function of the part. Is it a welded structural beam, a machined drive shaft, or a forged flange? If it is structural and heavily welded, you must narrow the candidates to structural grades (like S275JR or S355) that guarantee weldability and Charpy impact toughness. If it is a machined shaft requiring surface hardness, you must look at medium-to-high carbon engineering grades (like C45 or C50) that respond well to induction hardening or quenching and tempering.
Working through it as a series of questions can help. Is welding the primary fabrication method? If so, you need a structural grade with a low carbon equivalent (CEV) to prevent cracking. Is the part subject to dynamic loads or impact at low temperatures? If so, you need a grade with guaranteed Charpy V-notch impact values (e.g., 40 J at -20°C, typical for S460NL fine-grain steels). Is the part going to be heavily machined and subsequently hardened? If so, an engineering grade like C45 or C50 is required.
It’s tempting to reach for S235JR for everything because it is cheap and readily available, but structural service isn’t a single condition. The actual load, temperature, and fabrication method determine whether S235JR is sufficient or if S355 or S460 is required. Similarly, assuming any “C” grade will machine exactly the same way ignores the vast difference in chip formation and tool wear between C20 and C60.
The distinction worth remembering: you need grade selection when the service requirement is known but the material isn’t. You need specification selection when the material is already decided but the exact product still isn’t.
Carbon steel round-bar documents can carry several identifiers, and they do different jobs. A grade designation identifies the material chemistry, a product standard sets the requirements for the product itself, and dimensional or testing standards govern specific parts of the specification.
The same grade can appear under several designation systems depending on which document you’re reading:
| System | Example | Main purpose |
|---|---|---|
| EN (European) | C45 / 1.1191 | Standard European material designation |
| AISI / SAE | 1045 | Common American grade designation |
| Werkstoff | 1.1191 | German material number |
| JIS | S45C | Japanese designation |
The relevant product standards also do different jobs. Here’s a quick reference for what each one covers:
| Standard | Primary role |
|---|---|
| EN 10083-2 | Steels for quenching and tempering (Engineering steels like C45, C50) |
| EN 10025-2 | Non-alloy structural steels (S235JR, S275JR) |
| EN 10025-3 | Normalized/normalized rolled weldable fine grain steels (S460N) |
| ASTM A29/A29M | General requirements for carbon and alloy steel bars |
| ASTM A694 | High-strength forged fittings/flanges (e.g., F42) |
| EN 10060 | Hot-rolled round-bar dimensions and tolerances |
| EN 10278 | Bright steel-bar dimensions and tolerances |
| ISO 286-2 | Standard tolerance classes and limit deviations for holes and shafts |
| EN 10204 | Inspection-document types (e.g., 3.1 Certificate) |
Seeing EN 10083 and EN 10025 referenced together, it’s easy to assume they’re interchangeable. They aren’t. EN 10083 addresses engineering steels where hardenability, tensile strength, and machining are the focus. EN 10025 addresses structural steels where yield strength, weldability, and impact toughness are the focus. The lesson isn’t to memorize the numbers; it’s to identify which requirement each standard is actually performing. (ASTM International)
Before sending an enquiry, identify the material grade, record which designation system each document uses, identify the governing product standard, note any dimensional standard, identify the required testing standard, and verify that any equivalent grade mapping is actually accurate. Assuming EN 1.1191 (C45) and AISI 1045 are identical in every supply condition is a common trap; while chemically similar, their guaranteed mechanical properties depend entirely on the governing product standard and heat treatment applied by the mill.
Specify more than the nominal diameter whenever dimensional control actually matters. Dimensional tolerance is simply the permitted variation from a specified dimension, and the requirements that can matter go beyond diameter alone: diameter tolerance for machining and fit, length and length tolerance for fixed or cut components, straightness for shafts and precision work, and roundness or ovality for precision fits and rotating components.
The difference this makes in practice is easy to underestimate. A standard hot-rolled 50 mm bar might have a tolerance of +1.0 mm / -0.0 mm under EN 10060. A cold-drawn bright 50 mm bar to an h9 tolerance class under EN 10278 has a tolerance of just 0.062 mm. 50 mm on its own simply doesn’t communicate the same requirement as 50 mm h9. (BSSA)
What you actually need to specify depends on the job. General structural stock usually only needs diameter plus required length. Machining stock benefits from diameter, tolerance and the relevant surface condition (like peeled or turned). A precision shaft needs diameter, tight tolerance (like h8 or h9), straightness and roundness. A fixed-length component needs length and its applicable tolerance. And if you’re working from an existing drawing, match its dimensional and geometric requirements directly rather than reinventing them.
Straightness and roundness aren’t needed for every purchase. They matter specifically when geometry affects machining, assembly, rotation, feeding or component performance. Common mistakes here include assuming 50 mm means exactly 50.000 mm, when nominal size doesn’t define tolerance on its own; assuming diameter controls everything, when straightness and cross-sectional geometry are separate characteristics; and treating all tolerance classes as interchangeable.
Manufacturing and finishing should be chosen based on the dimensional and surface result the next operation actually needs. The manufacturing route is simply the production or finishing method used to bring the bar to its specified form and condition, and hot rolling, cold drawing, peeling, turning, grinding and forging each serve a different purpose.
Hot-rolled (black) bar is worth investigating when general structural use or heavy subsequent machining is sufficient. Cold-drawn (bright) bar matters when a controlled bright-bar condition, tighter dimensions and a better surface is genuinely required. Peeling is about controlled surface removal to eliminate the decarburized outer layer and surface defects of hot-rolled bar. Turning produces a machined outside diameter for larger diameters (often above 80mm where cold drawing isn’t feasible). Grinding adds further dimensional or surface precision on top of that. And forging-intended material is a separate category altogether, meant for material that will be forged rather than machined directly.
The practical way to decide: if the bar will undergo substantial machining after delivery, check whether conventional hot-finished material is actually sufficient before paying for more. If the delivered bar needs to be fed straight into an automatic lathe, look at cold-drawn or peeled bar to ensure consistent tool life and dimensional stability. If the outside diameter needs to be free of surface cracks and decarburization for induction hardening, peeling or turning is mandatory.
It’s not automatically better to buy the most highly finished bar available. Extra processing doesn’t add functional value if later machining is going to establish the final surface or dimension anyway. The better purchasing decision is the route that satisfies the required result without paying for unnecessary processing.
Heat-treatment condition fundamentally dictates the mechanical state of carbon steel. Unlike austenitic stainless steels, carbon steels are highly responsive to heat treatment, meaning grade, condition and required properties must be considered together. Material condition, in this context, means the metallurgical or supplied state of the product, including any relevant heat-treatment.
The most common supply conditions for carbon steel include:
Consider a C50 round bar. In the +N (normalized) condition, it is easier to machine. In the +QT (quenched and tempered) condition, that same C50 grade reaches higher yields (~520 MPa) with different toughness characteristics. The purchasing distinction worth remembering is that grade identifies the chemistry, while condition defines the mechanical state in which that chemistry is actually supplied.
The mechanical properties that typically matter are tensile strength, yield strength (especially critical for structural S-grades like S275JR at 275 MPa), elongation (ductility), and hardness. Additionally, for structural grades, Charpy V-Notch impact testing at specific temperatures (e.g., 27 Joules at +20°C for “JR”, or 40 Joules at -20°C for low-temp grades) is a vital property that dictates whether the steel will perform safely in cold environments.
Surface condition is also worth separating. Hot-rolled bars have a mill scale and a decarburized outer layer. If your application requires surface hardening (like induction hardening a C55 shaft), that decarburized layer must be removed via peeling or turning first, or the hardening process will fail.
Verification should connect the purchase requirement to the physical bar itself, its identification, and the evidence that supports it. An MTC (material test certificate) is only useful when it actually corresponds to the material supplied and the specification that applies.
The chain runs from requirement to order to identity to evidence to acceptance. The requirement establishes what was needed (grade, standard, dimensions, condition). The order becomes the contractual reference. The heat or material identification connects the physical product to its records. The chemistry, mechanical results and test certificate provide the evidence. And acceptance is where the physical product gets checked against both the order and that evidence.
For carbon steel, verifying the EN 10204 3.1 Certificate is standard practice. This document provides the specific inspection results for the delivered batch. You must verify that the chemical composition (Carbon, Manganese, Silicon, etc.) matches the grade, that the mechanical properties (Yield, Tensile, Elongation) meet the standard, and crucially, that any required impact test results (Charpy) are recorded at the correct temperature.
Working through verification is really a sequence of checks. Does the certificate grade match what was purchased? Can the material identity or heat number be matched to the physical bars (usually stamped or tagged on the bundle)? Do the dimensions match the order? Only once the physical material and its documentation genuinely correspond should you proceed to the normal receiving procedure. A heat number isn’t just paperwork; it’s what connects the material to its records, ensuring traceability from the steel mill to your final component.
Carbon steel round bars turn up across a wide range of industries, but the industry label should really only be a starting point. The component’s actual environment, manufacturing process, geometry and mechanical requirements are what determine the real product specification.
In general construction and structural frameworks, the main concern is weldability and yield strength, which points directly to S235JR or S275JR. For heavy-duty structural work or offshore applications where low-temperature impact is a risk, S460N or S460NL becomes necessary. For CNC machining of automotive or agricultural components, machinability and hardenability dominate, pointing to C45 or C50. For high-pressure oil and gas flanges and fittings, the combination of high yield strength (42 ksi / 290 MPa) and strict forging requirements points to grades like ASTM A694 F42.
Define the actual service environment, operating temperature, downstream manufacturing, dimensional and fit requirements, critical mechanical requirements and testing/documentation needs before selecting a grade from those constraints. It’s not safe to assume one grade can be used throughout a plant just because it’s familiar; a structural beam and a drive shaft in the same facility operate under completely different mechanical and fabrication conditions.
Build the specification in dependency order: material identity first, then manufacturing route, then geometry, then surface and condition, and finally evidence and delivery, since each stage depends on the one before it.
Start with the grade, designation and product standard (e.g., C45 to EN 10083-2), which establishes what material is actually being asked for. From there, define the manufacturing route (hot rolled, cold drawn, peeled, or turned). Next comes geometry: diameter (e.g., 6-250 mm), length, tolerance and any geometric controls. Then surface and condition: specify +N or +QT, and note if the surface must be free of decarburization. Finally, evidence and delivery: testing (EN 10204 3.1), traceability, packaging and destination.
A complete specification would cover the grade, governing product standard, manufacturing route, diameter and length, critical dimensional tolerances, straightness where needed, surface condition, material heat-treatment condition (+N, +QT), testing and certificate requirements, quantity, cut-to-length requirements, rust protection/packaging and destination.
C45 round bar, 50 mm on its own leaves standard, tolerance, route, condition, testing, and rust protection all essentially undefined. Working through the dependency chain stops critical decisions from staying implicit. A longer specification isn’t automatically a better one; the goal is enough relevant detail to remove the ambiguity that actually matters.
A good RFQ gives the supplier enough material, dimensional, condition, quality and delivery information to quote the intended product without having to make assumptions on your behalf.
It helps to compare what an incomplete request looks like against a more useful one. C45 round bar becomes more useful as C45 to EN 10083-2. 50 mm becomes 50 mm h9 tolerance, peeled. 10 pieces becomes 10 pieces, 3 meters each. Certified material becomes EN 10204 3.1 certificate with Charpy impact tests. Deliver to us becomes an actual destination plus requirement for VCI rust protection.
Before sending a request, state the grade, standard, diameter and length, quantity, tolerance and finish where required, material condition where applicable, certification and testing requirements, and destination and delivery requirement.
Ask honestly whether two qualified suppliers could reasonably interpret your RFQ differently. If so, clarify the missing specification. The lowest quoted price only means something once the technical scope behind it is actually comparable. Showing the fields a complete RFQ needs, rather than expecting a buyer to remember them from scratch, is really just an application of a basic usability principle: recognition is easier than recall. (Nielsen Norman Group)
Delivery requirements should cover cut length, product identification, rust protection, packaging, documentation and destination according to what the actual shipment needs.
Unlike stainless steel, carbon steel is highly susceptible to oxidation (rust) during transit and storage. Therefore, surface protection is not optional; it is a critical product requirement. Domestic and export shipments share most of the same categories, but export demands rigorous rust prevention. Length still needs to be defined, but identification needs to be maintained throughout the shipment. Documentation needs the applicable shipment paperwork on top of the usual 3.1 certificates. Packaging needs to be coordinated with the transport method to prevent physical damage and moisture ingress.
Before shipment, state the required length and any length tolerance, define surface protection (e.g., lightly oiled, VCI paper wrapped, or specific rust-preventative coatings), define bundle or product identification (heat numbers must remain visible), confirm the required technical documents, confirm packaging (wooden crates, steel strapping), and confirm the destination.
Whether fixed or exact length is required determines whether you need to state a tolerance alongside the length. Whether the shipment is international determines whether heavy-duty export packaging and VCI (Volatile Corrosion Inhibitor) wrapping apply. Leaving cut length until dispatch is a common mistake, since cutting is really a product requirement that belongs at the enquiry stage (e.g., utilizing “cut to size” services). Treating packaging as generic is another, since carbon steel will arrive rusted and unusable if moisture protection isn’t explicitly defined for transit.
The strongest buying decision isn’t simply the lowest price for a familiar grade. It’s the offer that describes the right material, production route, dimensions, condition and evidence for the intended service. Two supplier quotations are technically equivalent only when they describe the same relevant grade, product standard, dimensions, tolerance, condition, finish, testing/documentation and delivery requirements closely enough for their prices to actually be compared meaningfully.
It helps to think of the whole guide as a ladder. Why (what must the component survive) sets the service requirement. What (which material and standard satisfy it) sets the material identity. How (how it should be produced and finished) sets the manufacturing route. Exactly (what dimensions and condition are required) sets the physical specification. And prove it (how conformity will be established) sets the evidence.
A final purchasing diagnostic means covering service (load, welding, impact), material (grade, EN 10025 vs EN 10083), route (hot rolled, peeled, drawn), geometry (diameter, length, critical tolerances) and evidence (3.1 certificate, Charpy tests), in that order, before price ever enters the conversation.
Before comparing prices, check that both quotations are for the same material condition (+N vs +AR), that the same relevant product standard is being applied, that diameter and tolerances are equivalent, and that rust protection and delivery requirements are actually comparable. A lower price for an as-rolled bar when you actually need a normalized, peeled bar isn’t a lower price; it’s the wrong product.
A grade-and-price mindset asks who can supply S275JR the cheapest. A specification mindset asks whether the quotations are actually for equivalent products in the first place. The principle worth carrying forward: choose the material from the service requirement, define the product from the material and processing needs, and only compare suppliers once the quoted specifications are technically equivalent.
Send your carbon steel round bar grade, standard, dimensions, tolerances, condition, testing requirements, quantity and destination for quotation.
Tell us what you need and our sales team will get back to you with availability, pricing, and delivery options.