Alloy Steel 8620 Round Bar
Alloy Steel 8620 Round Bar manufacturer & supplier. Excellent case-hardening properties, wear resistance and core toughness for gears, shafts, pinions, camshafts and automotive transmission components. Enquire now.
Round Bars Wholesaler, Exporter & Supplier
Alloy steel round bars are solid cylindrical alloy-steel products used for high-temperature, high-pressure, and heavy-duty machined components, shafts, fasteners and refinery parts. But a grade and diameter alone don’t always define the complete product: a purchase may also need a product standard, length, manufacturing route, tolerance, surface finish, material condition, testing and documentation. ASTM A29/A29M and ASTM A322, for example, cover hot-wrought alloy steel bars, while grades like F22, F91 and B7 bring specific metallurgical requirements for elevated-temperature or bolting service.
Alloy Steel 8620 Round Bar manufacturer & supplier. Excellent case-hardening properties, wear resistance and core toughness for gears, shafts, pinions, camshafts and automotive transmission components. Enquire now.
Alloy Steel 30CrMo4 Round Bar manufacturer & supplier. High strength, toughness and hardenability for shafts, gears, axles, automotive components and demanding engineering applications. Enquire now.
Alloy Steel EN26 Round Bar manufacturer & supplier. High strength, toughness, hardenability and fatigue resistance for heavy-duty shafts, gears, axles and demanding engineering applications.
Alloy Steel EN31 Round Bar manufacturer & supplier. High hardness, wear resistance and rolling-contact fatigue strength for bearings, shafts, bushings and demanding engineering applications.
EN36 Round Bar manufacturer & supplier. Nickel-chromium case-hardening steel with a hard wear surface and very tough core for heavy-duty gears, camshafts and pinions. Enquire now.
Alloy Steel 35CrMo4 Round Bar manufacturer & supplier. High strength, toughness and hardenability for shafts, gears, axles, automotive components and demanding engineering applications. Enquire now.
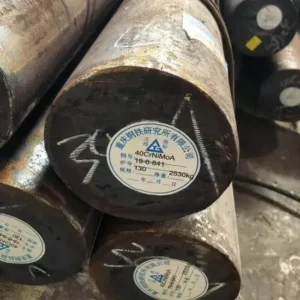
Alloy Steel 40CrNiMoA Round Bar manufacturer & supplier. High strength, toughness and hardenability for shafts, gears, axles, crankshafts and demanding automotive and heavy engineering applications. Enquire now.
Alloy Steel 35CrMoV Round Bar manufacturer & supplier. High strength, toughness and high-temperature resistance for shafts, fasteners, power generation, automotive and heavy engineering applications.
Alloy Steel 12Cr1MoV Round Bar manufacturer & supplier. High-temperature strength, creep resistance and oxidation resistance for boilers, steam turbines, power generation and demanding industrial applications.
Alloy Steel 15CrMo Round Bar manufacturer & supplier. Good strength, toughness and high-temperature performance for gears, shafts, pins, pressure components and demanding engineering applications.
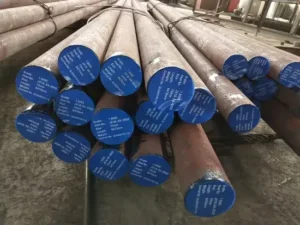
Alloy Steel 20CrMo Round Bar manufacturer & supplier. Good strength, toughness and hardenability for gears, shafts, axles, pins and demanding automotive and engineering applications. Enquire now.
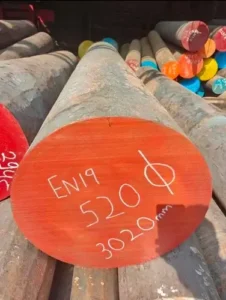
Alloy Steel EN19 Round Bar manufacturer & supplier. High strength, toughness and hardenability for shafts, gears, axles, bolts and demanding automotive and engineering applications. Enquire now.
An alloy steel round bar is a solid cylindrical alloy-steel bar supplied to defined material, dimensional, condition and quality requirements. It helps to think about a purchase like this in five stages: first the service requirement the part has to survive (often high temperature, high pressure, or severe mechanical stress), then the material and governing standard that satisfy it, then the production route used to make it, then the exact geometry and condition needed, and finally the testing and documentation that prove all of that was actually delivered.
An alloy steel round bar is a solid cylindrical alloy-steel product, and its complete specification can include its grade, product standard, diameter, length, manufacturing route, tolerance, surface finish, material condition and required documentation. The product specification, in practice, is the complete set of technical and commercial requirements that determines what a supplier is expected to deliver.
Nine things typically define the product. The grade establishes the material identity. The product standard identifies the governing specification. Diameter sets the intended cross-sectional size, and length determines how the bar is prepared and handled. The manufacturing route can affect dimensional and surface characteristics. Tolerance defines the acceptable dimensional deviation. Surface finish affects machining and downstream use. Material condition affects which mechanical requirements apply. And testing or documentation supports conformity and acceptance.
Consider a request for an ASTM A182 F22 alloy steel round bar, 50 mm. That identifies the grade and nominal diameter, but it doesn’t tell the supplier which product standard governs the bar itself, what length is required, what tolerance is acceptable, what surface finish is needed, what heat-treatment condition is required, or what certification and testing is expected.
Before sending an enquiry, define the application, record the required grade, identify the product standard, note diameter and length, define any critical tolerance or finish, state the required heat treatment and documentation, and confirm quantity and destination.
The most common mistake is treating grade plus diameter as a complete specification. Important supply requirements get left undefined that way, so it helps to complete the relevant fields rather than assume a 50 mm bar from one supplier matches a 50 mm bar from another (tolerance and heat-treatment condition can differ significantly). It also helps to resist copying a supplier’s entire specification table into an RFQ. Not every field they list will be relevant to your part, so specify only what actually affects the product you need.
Alloy steel round bars are available across a number of metallurgical families: Carbon-Molybdenum (C-Mo), Chromium-Molybdenum (Cr-Mo), Creep Strength Enhanced Ferritic/Martensitic (CSEF), Nickel-Chromium-Molybdenum (Ni-Cr-Mo) and dedicated bolting grades. They differ in structure and in the combinations of high-temperature strength, creep resistance, hydrogen attack resistance and heat-treatment response they offer. A grade family, in other words, is a group of alloy steels with related metallurgical structures and broadly related properties.
C-Mo grades like F1 are usually chosen for moderate-temperature strength and cost-efficiency in piping parts. Cr-Mo grades such as F5, F9, F11, F12 and the widely used F22 (2.25Cr-1Mo) are picked for their oxidation resistance, creep strength, and suitability for refinery and boiler service. CSEF grades, like F91 (9Cr-1Mo-V) and F92 (9Cr-W-Mo-V-Nb), are selected for advanced, ultra-supercritical power plant duty where extreme high-temperature strength is required. Ni-Cr-Mo grades like 8630 combine high hardenability with toughness for pressure-containing components, and dedicated bolting grades such as B7 (Cr-Mo) and B16 (Cr-Mo-V) are used where specific high-tensile fastener conditions are needed. (Specialty suppliers also frequently stock high-performance alloys like Super Duplex Zeron 100 alongside these grades for extreme chloride environments).
Within these families, F11 and F22 are the standard power piping and refinery grades. F91 and F92 are the advanced high-temperature options. B7 is the standard quenched and tempered bolting grade, while B16 is rated for higher service temperatures. 8630 is the common choice for wellhead equipment.
One assumption is worth being cautious about: the most common grade isn’t automatically the right grade. A familiar grade is only a candidate; the application determines which requirements actually matter. If you know the application but not the grade, the next section walks through a selection method. If you already know the grade but not the exact product form, skip ahead to the standards and specification sections.
Grade selection should start with the conditions the component actually has to withstand, then narrow the candidates by temperature, fabrication and mechanical requirements. That’s what a service requirement really is: the environmental, thermal, fabrication and mechanical conditions the component must accommodate.
This approach works best when you know the application but aren’t sure of the grade yet. Start with the environment the bar will encounter, since that narrows the corrosion and service candidates fastest. Then consider temperature, which narrows thermal-use candidates, followed by how the part will be machined, welded or formed, which adds fabrication constraints. Add in the strength or hardness the part demands, and by that point you should have a short list of realistic candidates. Where their requirements conflict with each other, weigh the trade-offs to land on the practical choice.
Working through it as a series of questions can help. Is elevated temperature or creep the dominant constraint? If so, narrow by high-temperature grades first; if not, move on to pressure and fabrication. Is hydrogen service a factor? If yes, resistance to High-Temperature Hydrogen Attack (HTHA) dictates the chromium and molybdenum content (e.g., using F22 or F91 instead of carbon steel, per API RP 941 Nelson Curves). Is the part a high-tensile fastener? If so, hardenability and impact toughness need to be part of the comparison. Is strength or hardness critical? If so, include heat-treatable candidates where they apply. And if the requirements still conflict at that point, compare what’s left by trade-off rather than defaulting to habit.
It’s tempting to reach for F22 as soon as elevated temperature comes up, but high-temperature service isn’t a single condition. The actual operating temperature, pressure, hydrogen exposure, and mechanical duty still determine whether F22 is the right call. Shortcuts like refinery means F22 or power plant means F91 can be useful starting points, but they’re not complete material-selection rules on their own.
The distinction worth remembering: you need grade selection when the service requirement is known but the material isn’t. You need specification selection when the material is already decided but the exact product still isn’t.
Alloy steel round-bar documents can carry several identifiers, and they do different jobs. A grade designation identifies the material, a product standard sets the requirements for the product itself, and dimensional or testing standards govern specific parts of the specification. A product standard, formally, is a technical specification that establishes requirements for a defined class of products.
The same grade can appear under several designation systems depending on which document you’re reading:
| System | Example | Main purpose |
|---|---|---|
| AISI/SAE | 4140 / 8630 | Common alloy grade designation |
| ASTM Grade | F22 / F91 / B7 | Specification for high-temp or bolting service |
| EN / Werkstoff | 1.7380 / 1.4903 | European material designation |
| UNS | K21590 / K90901 | Unified alloy identification |
The relevant product standards also do different jobs. Here’s a quick reference for what each one covers:
| Standard | Primary role |
|---|---|
| ASTM A29/A29M | Hot-wrought carbon and alloy steel bars (General requirements) |
| ASTM A322 | Hot-wrought alloy steel bars (Specific composition ranges) |
| ASTM A182/A182M | Forged/rolled alloy parts (Often specified for F-grade chemistry) |
| ASTM A193/A193M | Alloy-steel bolting for high-temp/high-pressure (Covers B7, B16) |
| ASTM A370 | Mechanical testing methods and definitions |
| EN 10083-3 | Technical delivery conditions for alloy steels |
| EN 10204 | Metallic products – Types of inspection documents |
ASTM explicitly distinguishes A29 (general bars) from A182 (forgings/fittings) and A193 (bolting). Seeing A182, A29 and A193 referenced together, it’s easy to assume they’re interchangeable. They aren’t. A29 addresses general hot-wrought alloy steel bars. A193 addresses alloy-steel materials specifically intended for high-temperature or high-pressure bolting (which covers B7 and B16). A182 addresses forged or rolled parts like flanges and fittings. Buyers frequently specify “A182 F22 round bar” to lock in the strict chemistry and melting practices of the F22 grade, even if the physical product is a wrought bar governed dimensionally by A29 or A322. The lesson isn’t to memorize three numbers; it’s to identify which requirement each standard is actually performing.
Designation mapping matters the same way. 10CrMo9-10 maps to F22, to EN 1.7380, to UNS K21590, while X10CrMoVNb9-1 maps to F91, to EN 1.4903, multiple names for related alloys, which is exactly why checking each document’s role matters rather than assuming the numbers explain themselves.
Before sending an enquiry, identify the material grade, record which designation system each document uses, identify the governing product standard, note any dimensional standard, identify the required testing standard, and verify that any equivalent grade mapping is actually accurate. A few mistakes are worth avoiding: treating every ASTM or EN reference as if it were the material standard, when some govern dimensions, tests or treatments instead; assuming equivalent grades mean identical specifications, when cross-designations don’t erase product-standard differences; and listing every standard you’ve come across without stating which one actually applies, since the supplier still has to interpret the order either way.
Specify more than the nominal diameter whenever dimensional control actually matters. Dimensional tolerance is simply the permitted variation from a specified dimension, and the requirements that can matter go beyond diameter alone: diameter tolerance for machining and fit, length and length tolerance for fixed or cut components, straightness for shafts and precision work, and roundness or ovality for precision fits and rotating components.
The difference this makes in practice is easy to underestimate. 20 mm on its own simply doesn’t communicate the same requirement as 20 mm h9.
What you actually need to specify depends on the job. General stock usually only needs diameter plus required length. Machining stock benefits from diameter, tolerance and the relevant surface condition. A precision fit needs diameter, tolerance, straightness and roundness/ovality where they matter. A fixed-length component needs length and its applicable tolerance. And if you’re working from an existing drawing, match its dimensional and geometric requirements directly rather than reinventing them.
Straightness and roundness aren’t needed for every purchase. They matter specifically when geometry affects machining, assembly, rotation, feeding or component performance, so it’s worth checking whether any of those apply before adding them to a spec. Common mistakes here include assuming 20 mm means exactly 20.000 mm, when nominal size doesn’t define tolerance on its own; assuming diameter controls everything, when straightness and cross-sectional geometry are separate characteristics that need adding when the application requires them; and treating all tolerance classes as interchangeable, when different classes permit very different limits.
Manufacturing and finishing should be chosen based on the dimensional and surface result the next operation actually needs. The manufacturing route is simply the production or finishing method used to bring the bar to its specified form and condition, and hot rolling, forging, cold drawing, peeling, turning and grinding each serve a different purpose.
Hot-rolled bar is worth investigating when general stock or subsequent machining is sufficient. Forged bar matters when large diameters or critical pressure components require refined grain structures and directional strength. Cold-drawn (bright) bar matters when a controlled bright-bar condition, tighter dimensions and a better surface, is genuinely required. Peeling is about controlled surface removal for size and surface refinement. Turning produces a machined outside diameter. Grinding adds further dimensional or surface precision on top of that. And forging-intended material is a separate category altogether, meant for material that will be forged rather than machined directly.
The practical way to decide: if the bar will undergo substantial machining after delivery, check whether conventional hot-rolled material is actually sufficient before paying for more. If the delivered bar needs controlled bright-bar dimensions from the outset, look at the appropriate bright-bar route and tolerance. If the outside diameter needs refining, peeling or turning are the options; if it needs further dimensional or surface finishing on top of that, grinding is the next step. And if the material is specifically intended for forging, that’s a distinct requirement to verify directly rather than assume.
It’s not automatically better to buy the most highly finished bar available. Extra processing doesn’t add functional value if later machining is going to establish the final surface or dimension anyway. The better purchasing decision is the route that satisfies the required result without paying for unnecessary processing.
Heat-treatment condition is arguably the most critical variable for alloy steel, as it directly dictates the mechanical state of applicable grades, while surface finish and chemical surface treatment address entirely different characteristics. That means grade, condition and required properties need to be considered together rather than in isolation. Material condition, in this context, means the metallurgical or supplied state of the product, including any relevant heat-treatment or cold-work condition.
F91 is a useful example. It combines high-temperature creep strength with improved thermal conductivity compared to older Cr-Mo grades. But the purchasing distinction worth remembering is that grade identifies the alloy, while heat-treatment condition defines the state in which that alloy is actually supplied. F91 requires a highly specific austenitizing and tempering cycle to achieve its tempered martensite structure; if supplied in the wrong condition, it will fail in service. Similarly, B7 must be quenched and tempered to achieve its required tensile strength.
The mechanical properties that typically matter are tensile strength (the maximum tensile stress reached in testing, used for load-bearing evaluation), yield strength (the stress associated with the onset of plastic deformation, used in design and load evaluation), elongation (a measure tied to ductility, relevant to forming and deformation), and hardness (resistance to indentation, relevant to wear and application requirements). Crucially, for alloy steels, creep rupture strength and Charpy impact toughness are often the defining properties for high-temperature or high-pressure service.
Surface finish and protection are also worth separating clearly. A machined finish is a surface-finish requirement, while rust prevention is a distinct surface treatment. Alloy steels lack the passive chromium-oxide layer of stainless steels, meaning they will oxidize and rust rapidly if exposed to moisture during transit.
Before finalizing a spec, confirm the required grade and material condition, identify the critical mechanical properties, specify surface finish where relevant, and specify rust prevention separately where it’s required, along with whatever tests or documentation apply. Grade alone doesn’t guarantee every delivered property; condition and specification matter too. Property tables aren’t universal either, since values depend on grade, condition and the governing specification, so use the applicable standard rather than a generic reference. A buyer who compares only grade and tensile strength can still miss whether the delivered condition actually suits the component, which is why grade, condition, required property and verification are best treated as one connected chain rather than four separate checks.
Verification should connect the purchase requirement to the physical bar itself, its identification, and the evidence that supports it. An MTC (material test certificate) is only useful when it actually corresponds to the material supplied and the specification that applies. Material traceability, in this sense, is the ability to connect supplied material back to its production or heat identification and the records associated with it.
The chain runs from requirement to order to identity to evidence to acceptance. The requirement establishes what was needed (grade, standard, dimensions, condition). The order becomes the contractual reference. The heat or material identification connects the physical product to its records. The chemistry, mechanical results and test certificate provide the evidence. And acceptance is where the physical product gets checked against both the order and that evidence.
Ultrasonic Testing (UT) is highly relevant for large-diameter alloy bars (like F91 or 8630) to detect internal voids or inclusions before machining. Charpy V-Notch testing ensures impact toughness. High-temperature tensile testing verifies creep properties. EN 10204 defines the types of inspection documents (e.g., 3.1 or 3.2 certificates) that provide this evidence.
Working through verification is really a sequence of checks. Does the certificate grade match what was purchased? If not, stop and resolve the discrepancy before going further. Can the material identity or heat number be matched? If not, traceability hasn’t actually been established. Do the dimensions match the order? Do the chemistry, mechanical and test results satisfy the governing requirement? Only once the physical material and its documentation genuinely correspond should you proceed to the normal receiving procedure.
In practice that means matching the purchased grade and governing standard, matching the heat or material identification, checking the required chemistry and mechanical results, checking dimensions and condition, checking the inspection and testing records, and confirming traceability all the way through receiving. Getting an MTC from a supplier isn’t the end of the process. The document is evidence, not a substitute for matching it to the physical material and the purchase requirement. A heat number isn’t just paperwork either; it’s what connects the material to its records, so the physical and documentary checks need to be closed together rather than treated as separate boxes.
Alloy steel round bars turn up across a wide range of industries, but the industry label should really only be a starting point. The component’s actual environment, manufacturing process, geometry and mechanical requirements are what determine the real product specification. An application requirement, defined more precisely, is the service and manufacturing conditions imposed by the component’s intended use.
In power generation, the main concern is long-term creep strength and thermal fatigue, which usually means paying close attention to CSEF grades like F91 and F92, along with strict heat-treatment verification. For oil and gas refineries, High-Temperature Hydrogen Attack (HTHA) dominates: the chromium and molybdenum content must be matched to the Nelson curve limits for the specific operating temperature and hydrogen partial pressure (favoring F5, F9, or F22). Wellhead and Christmas tree equipment adds high-pressure and sour-gas requirements, bringing grades like 8630 and API 6A compliance into play. And high-tensile bolting applications are governed by the need for specific yield strengths and impact toughness, which is why B7 and B16 have their own dedicated standards.
Define the actual service environment, operating temperature, downstream manufacturing, dimensional and fit requirements, critical mechanical requirements and testing/documentation needs before selecting a grade from those constraints, rather than the other way around. It’s not safe to assume one grade can be used throughout a plant just because it’s familiar; components in the same facility can operate under very different temperatures, environments, loads and manufacturing conditions. An industry name like refinery service, power generation or wellhead equipment describes a context, not a complete material requirement on its own.
Build the specification in dependency order: material identity first, then manufacturing route, then geometry, then surface and condition, and finally evidence and delivery, since each stage depends on the one before it. A purchase specification, in full, is the complete technical description used to tell a supplier exactly what product is required.
Start with the grade, designation and product standard, which establishes what material is actually being asked for. From there, define the manufacturing route (hot rolled, forged, cold drawn, peeled, turned, ground, or forging-intended, whichever applies), since that defines the supply route itself. Next comes geometry: diameter, length, tolerance and any geometric controls that matter. Then surface and condition: finish, roughness where relevant, and material condition or heat treatment, which together define the state the bar is delivered in. Finally, evidence and delivery: testing, certification, traceability, packaging and destination, which define how conformity will be verified and how the material will actually arrive.
A complete specification would cover the grade, designation, governing product standard, manufacturing route where relevant, diameter and length, critical dimensional tolerances, straightness/roundness where needed, surface finish, heat-treatment condition, rust prevention where required, testing and certificate requirements, inspection requirements, quantity, cut-to-length requirements, packaging and destination.
It’s a useful exercise to see the transformation directly. F22 round bar, 50 mm on its own leaves grade, standard, diameter, length, tolerance, route, finish, condition, testing/certificate, quantity and delivery all essentially undefined. Not every field will be relevant to every order; the exact fields depend on the application, but the purpose of working through them is to stop critical decisions from staying implicit.
If the grade itself is still unknown, go back to the service-constraint approach earlier in this guide. If the grade is known but the product is still incomplete, work through this dependency chain. And if supplier quotations come back looking different from each other, apply the purchase-to-proof logic from the testing section and compare the complete specifications side by side rather than just the prices.
A longer specification isn’t automatically a better one. The goal isn’t maximum detail; it’s enough relevant detail to remove the ambiguity that actually matters. Adding fields that don’t affect the purchase just adds noise. Copying a supplier’s own table can pull in requirements that aren’t actually essential. And leaving critical fields implicit invites different suppliers to interpret them differently, which is exactly what a specification is meant to prevent.
A good RFQ gives the supplier enough material, dimensional, condition, quality and delivery information to quote the intended product without having to make assumptions on your behalf. At minimum, an RFQ needs the grade, designation and governing standard on the material side; diameter, length and quantity on the geometry side; manufacturing route, finish, tolerance and heat-treatment condition where they apply, for product condition; certificate, testing and inspection requirements for quality evidence; and cut-to-length, packaging, destination and delivery requirements for the delivery side.
It helps to compare what an incomplete request looks like against a more useful one. F22 round bar becomes more useful as grade plus governing standard. 50 mm becomes diameter plus required tolerance. 10 pieces becomes quantity plus length. Certified material becomes a defined certificate or testing requirement. Deliver to us becomes an actual destination plus delivery requirement.
Before sending a request, state the grade, standard, diameter and length, quantity, tolerance and finish where required, heat-treatment condition where applicable, certification and testing requirements, inspection requirements, and destination and delivery requirement.
Ask honestly whether two qualified suppliers could reasonably interpret your RFQ differently. If so, clarify the missing specification before you send it out, since an RFQ that leaves room for interpretation is much less likely to produce quotations you can actually compare. A supplier can certainly help identify missing requirements, but critical engineering requirements shouldn’t be left to supplier guesswork by default. And the lowest quoted price only means something once the technical scope behind it is actually comparable; price becomes meaningful after that point, not before it. Showing the fields a complete RFQ needs, rather than expecting a buyer to remember them from scratch, is really just an application of a basic usability principle: recognition is easier than recall.
Delivery requirements should cover cut length, product identification, protection, packaging, documentation and destination according to what the actual shipment needs. Cut-to-length simply means supplying bar material at a specified customer-required length.
Domestic and export shipments share most of the same categories, but export tends to demand more of each. Length still needs to be defined either way, but identification needs to be maintained throughout the shipment rather than just where required. Surface protection needs to account for longer transport and handling. Documentation needs the applicable shipment paperwork on top of the usual specification documents. Packaging needs to be coordinated with the transport method and destination rather than just matched to local handling. And traceability needs to be maintained through shipment and receipt, not just at the point of dispatch.
Alloy steels lack the passive chromium-oxide layer of stainless steels, meaning they will oxidize and rust rapidly if exposed to moisture during transit. Surface protection is not optional; it requires defined rust preventatives, VCI (Volatile Corrosion Inhibitor) wrapping, and heavy-duty wooden or steel crating for export.
Before shipment, state the required length and any length tolerance, define surface protection and rust prevention, define bundle or product identification, confirm the required technical documents, confirm packaging, confirm the destination, confirm any applicable export documents, and maintain traceability through the whole shipment.
Whether fixed or exact length is required determines whether you need to state a tolerance alongside the length, or simply confirm an acceptable supply length. Whether the surface is sensitive to handling determines whether protection requirements need to be defined, or whether standard packaging is enough. And whether the shipment is international determines whether destination-specific documentation and packaging apply, or whether the usual domestic delivery requirements will do.
Packaging isn’t purely a logistics issue. Protection, identification and documentation can all affect receiving, inspection and traceability once the material arrives. Leaving cut length until dispatch is a common mistake, since cutting is really a product requirement that belongs at the enquiry stage, not an afterthought. Treating packaging as generic is another, since product and transport conditions differ enough to need a defined protection requirement. And separating documents from delivery causes problems too, since receiving teams need the evidence tied to the material, not delivered separately from it.
The strongest buying decision isn’t simply the lowest price for a familiar grade. It’s the offer that describes the right material, production route, dimensions, condition and evidence for the intended service. Two supplier quotations are technically equivalent only when they describe the same relevant grade, product standard, dimensions, tolerance, condition, finish, testing/documentation and delivery requirements closely enough for their prices to actually be compared meaningfully.
It helps to think of the whole guide as a ladder. Why (what must the component survive) sets the service requirement. What (which material and standard satisfy it) sets the material identity. How (how it should be produced and finished) sets the manufacturing route. Exactly (what dimensions and condition are required) sets the physical specification. And prove it (how conformity will be established) sets the evidence.
A final purchasing diagnostic means covering service (environment, temperature, component duty), material (grade, governing standard), route (manufacturing route, required finish), geometry (diameter, length, critical tolerances) and evidence (testing/certification, traceability requirements), in that order, before price ever enters the conversation.
Before comparing prices, check that both quotations are for the same material, that the same relevant product standard is being applied, that diameter, length and tolerances are equivalent, that manufacturing and material conditions match, that the surface requirement is equivalent, that testing and documentation requirements match, and that quantity, destination and delivery requirements are actually comparable.
The lowest price is only the most important factor once the relevant technical scope is comparable. A lower price for a different tolerance, finish, condition or documentation requirement isn’t actually a lower price for the same product; it’s a different product. Comparing price first and resolving technical differences later gets the order backwards.
A grade-and-price mindset asks who can supply F22 the cheapest. A specification mindset asks whether the quotations are actually for equivalent products in the first place, and the second question is more useful, because an alloy steel round bar was never fully defined by its grade name alone. The principle worth carrying forward: choose the material from the service requirement, define the product from the material and processing needs, and only compare suppliers once the quoted specifications are technically equivalent.
Send your alloy steel round bar grade, standard, dimensions, tolerances, heat-treatment condition, testing requirements, quantity and destination for quotation.
Tell us what you need and our sales team will get back to you with availability, pricing, and delivery options.