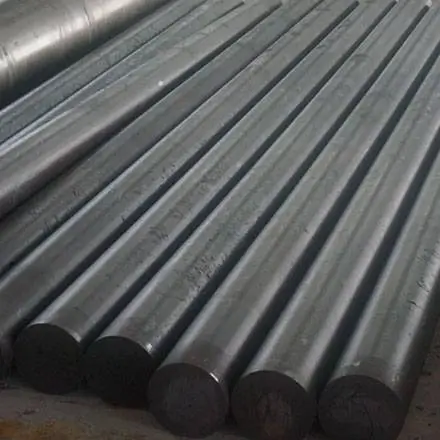
Alloy Steel F92 Round Bar
➡️ ASTM A182 F92 | UNS K92460 | EN 1.4901
➡️ ASTM, EN, JIS & International Standards
➡️ Supply Conditions
➡️ Multiple Diameters & Supply Lengths
➡️ Global Export & International Delivery
Country of Origin:
Europe, Japan, USA
Material Type:
Alloy Steel
UNS Number:
K92460
Wr. No.:
1.4901
MTC Available:
EN 10204 3.1
Product Description for Alloy Steel F92 Round Bar
Alloy Steel F92 Round Bar is bar or forged round stock produced to ASTM A182 / A182M Grade F92, the specification covering forged alloy and stainless steel piping components for high-temperature service. The ASME designation is SA182 F92 and the UNS number is K92460. It is a creep-strength-enhanced ferritic steel of the 9Cr-2W type, developed as an improvement on Grade F91 for advanced and ultra-supercritical power plant.
The composition combines 8.50-9.50% chromium with 1.50-2.00% tungsten, 0.30-0.60% molybdenum, controlled vanadium, niobium and nitrogen, and a small boron addition of 0.001-0.006%. Tungsten and boron together push creep rupture strength well above F91 at temperatures around 600-620 deg C. That allows thinner pipe walls, lighter components and less thermal fatigue in plant that cycles.
Material is supplied normalised and tempered, normalised typically at 1040-1080 deg C and tempered at 730-800 deg C, producing a tempered martensitic structure. Mandatory mechanical requirements are 620 MPa minimum tensile strength, 440 MPa minimum yield strength, 20% minimum elongation and 45% minimum reduction of area, with a maximum hardness of 269 HBW.
Bar is available in diameters from about 25 mm to 500 mm in 3 to 6 m lengths. Welding requires strict control of preheat, interpass temperature and post-weld heat treatment, since incorrect PWHT causes severe loss of creep strength in the heat-affected zone.
Typical applications include main steam and hot reheat piping flanges and fittings, valve bodies and bonnets, headers, turbine components and boiler pressure parts. Industries served include power generation, particularly supercritical and ultra-supercritical coal plant, petrochemical and heavy process industries.
Common Applications of Alloy Steel F92 Round Bar
➡️ Machined shafts, spindles, valve stems, pump sleeves and pins for food, beverage, dairy and pharmaceutical equipment, where the passive chromium oxide film resists both product acids and caustic clean-in-place chemicals.
➡️ Fasteners, studs, bolts, threaded rod and anchor components produced from bar stock, chosen for corrosion resistance combined with the ductility needed for cold heading and thread rolling.
➡️ Chemical, water treatment and general process plant parts such as agitator shafts, flange blanks, nozzles and support components handling water, steam and mildly corrosive media free of significant chlorides.
➡️ Architectural and structural hardware including handrail stanchions, balustrade fittings, tension rods and bollards, where a bright ground or polished bar finish provides both appearance and low maintenance.
International Equivalent Grade for AS F92 Round Bar
Standard
Country / Region
Grade
ASTM A182 / A182M
USA
Grade F92 (UNS K92460)
ASME SA182 / SA182M
USA
SA182 F92
EN 10222-2
Europe / EU
X10CrWMoVNb9-2 (1.4901)
BS EN 10222-2
United Kingdom
X10CrWMoVNb9-2 (1.4901)
GB/T 5310
China
10Cr9MoW2VNbBN
Technical Specification for Alloy Steel F92 Round Bar
Specification
Value
Unit
Material
Creep-strength-enhanced ferritic alloy steel
-
Grade
F92 / UNS K92460 / X10CrWMoVNb9-2
-
Product Form
Round bar / forged round / forging stock
-
Standard
ASTM A182 / A182M and ASME SA182
-
Diameter
25 - 500 (available range)
mm
Length
3 - 6 (standard random or fixed)
m
Manufacturing Process
Forged, or hot rolled and machined
-
Production Route
EAF melting with ladle refining and vacuum degassing, optional ESR remelting, forging, normalising and tempering
-
Surface Finish
As-forged and descaled, hot-rolled black, peeled, rough turned, machined
-
Heat Treatment / Delivery Condition
Normalised and tempered (mandatory per ASTM A182)
-
Normalising Temperature
1040 - 1080 then air cool (typical)
deg C
Tempering Temperature
730 - 800 (typical)
deg C
Typical Design Service Temperature Range
565 - 620
deg C
Preheat Temperature for Welding
200 - 300 (typical)
deg C
Post-Weld Heat Treatment
730 - 770 (typical, mandatory for welded joints)
deg C
Tolerance Standard
ASTM A29 / A29M for bar dimensions
-
Density
7.76 (typical)
g/cm3
Melting Range
1420 - 1470 (approximate)
deg C
Thermal Conductivity
26.0 at 100 deg C (typical)
W/m.K
Coefficient of Thermal Expansion
11.0 at 20 - 300 deg C (typical)
micro-m/m.K
Specific Heat
480 at 20 - 100 deg C (typical)
J/kg.K
Electrical Resistivity
0.60 (typical)
micro-ohm.m
Modulus of Elasticity
213 at room temperature (typical)
GPa
Magnetic Properties
Ferromagnetic
-
Applicable Testing Standard
ASTM A370, ASTM E8 / E8M, ASTM E23, ASTM E10, ASTM E415, ASTM A788
-
Certification / Inspection Documents
EN 10204 Type 3.1 or 3.2 mill test certificate
-

Technical Specifications
Get the key technical specifications for Alloy Steel F92 Round Bar
Alloy Steel F92 Round Bar is governed by ASTM A182 / A182M, adopted by ASME as SA182, with ASTM A788 / A788M providing general requirements for steel forgings.
Heat treatment is mandatory and tightly controlled. Normalising is carried out at approximately 1040-1080 deg C to dissolve carbides and take vanadium, niobium and nitrogen into solution, followed by air cooling to produce a fully martensitic structure. Tempering at 730-800 deg C then precipitates fine MX carbonitrides and M23C6 carbides, which are the particles that pin dislocations and deliver the creep strength.
Both the normalising and tempering temperatures matter. Normalising too low leaves carbides undissolved and reduces creep life, while tempering above the lower critical temperature produces fresh untempered martensite that is brittle and must be corrected by full re-heat treatment.
Welding requires the most careful control of any grade in the A182 family. Preheat of 200-300 deg C is required, the joint must be cooled to about 80-100 deg C before post-weld heat treatment to complete the martensitic transformation, and PWHT is then performed at 730-770 deg C. Incorrect PWHT causes type IV cracking in the fine-grained heat-affected zone, which is the dominant in-service failure mechanism for this family of steels.
Testing includes analysis to ASTM E415, tensile testing to ASTM A370 and E8 / E8M, hardness to ASTM E10 and, where specified, Charpy testing to ASTM E23 and ultrasonic examination to ASTM A388.
Chemical Composition for Alloy Steel F92 Round Bar
Element
Symbol
Min
Max
Unit
Carbon
C
0.07
0.13
%
Manganese
Mn
0.30
0.60
%
Silicon
Si
-
0.50
%
Phosphorus
P
-
0.020
%
Sulfur
S
-
0.010
%
Chromium
Cr
8.50
9.50
%
Molybdenum
Mo
0.30
0.60
%
Tungsten
W
1.50
2.00
%
Vanadium
V
0.15
0.25
%
Niobium
Nb
0.04
0.09
%
Nitrogen
N
0.030
0.070
%
Boron
B
0.001
0.006
%
Nickel
Ni
-
0.40
%
Aluminium
Al
-
0.020
%
Titanium
Ti
-
0.010
%
Zirconium
Zr
-
0.010
%
Iron
Fe
Balance
Balance
%

Chemical Composition
View the chemical composition and applicable material limits for AS F92 Round Bar
Chromium at 8.50-9.50% provides oxidation and steam-side corrosion resistance at service temperature and contributes to the stability of the tempered martensitic matrix. Nine percent is the practical optimum, high enough for good steam oxidation resistance without forming delta ferrite.
Tungsten at 1.50-2.00% is what separates F92 from F91. It is a strong solid solution strengthener that diffuses slowly, so it holds the martensitic substructure together against softening and recovery over long exposure. Paired with a reduced molybdenum content of 0.30-0.60%, it lifts creep rupture strength at 600-620 deg C well above F91.
Three more elements work as a set. Vanadium at 0.15-0.25%, niobium at 0.04-0.09% and nitrogen at 0.030-0.070% form very fine, stable MX carbonitride precipitates during tempering. These particles pin dislocations and sub-grain boundaries and are the principal source of long-term creep strength.
The boron addition, only 0.001-0.006%, matters more than its size suggests. It segregates to boundaries and stabilises the M23C6 carbides against coarsening, extending creep life. Aluminium, titanium and zirconium are strictly capped because they tie up nitrogen as nitrides and prevent it from forming the beneficial MX particles.
Carbon at 0.07-0.13% is kept low for weldability, and phosphorus and sulphur are held to 0.020% and 0.010% to protect creep ductility and toughness.
Mechanical Properties for Alloy Steel F92 Round Bar
Mechanical Property
Value
Unit
Tensile Strength
620 (minimum)
MPa
Yield Strength 0.2% Proof
440 (minimum)
MPa
Elongation in 50 mm
20 (minimum)
%
Reduction of Area
45 (minimum)
%
Hardness
269 max
HBW
Impact / Charpy V-Notch
Not required by ASTM A182 unless specified as a supplementary requirement
J
Modulus of Elasticity
213 at room temperature (typical)
GPa

Mechanical Properties
Check the key mechanical properties and performance requirements of AS F92 Round Bar
ASTM A182 / A182M imposes mandatory room-temperature mechanical requirements on Grade F92: a minimum tensile strength of 620 MPa, minimum yield strength of 440 MPa, 20% minimum elongation in 50 mm, 45% minimum reduction of area, and a maximum hardness of 269 HBW. Testing follows ASTM A370 and ASTM E8 / E8M, with hardness to ASTM E10.
A182 specifies hardness for F92 as a maximum only, unlike Grade F91 which carries a two-sided band of 190-248 HBW. A reading above 269 HBW indicates under-tempering and a risk of brittle behaviour and is cause for rejection or re-heat treatment. Over-tempering is not caught by the hardness requirement alone, so the tensile and yield minima do the work at the low end. Many owner specifications add a hardness floor of about 190 HBW as a supplementary requirement, precisely because low hardness correlates with reduced creep strength in service.
Room-temperature values are not the design basis for this grade. F92 is selected for creep rupture strength between roughly 565 and 620 deg C, and design uses the allowable stresses tabulated in the ASME Boiler and Pressure Vessel Code and ASME B31.1, which are governed by 100 000 hour creep rupture data.
Charpy impact testing is not mandatory under A182 but is commonly invoked, since the fine-grained heat-affected zone of welded joints in this family is where type IV creep cracking initiates.
Dimension / Sizes for Alloy Steel F92 Round Bar
Dimension / Size
Value
Unit
Diameter (available range)
25 - 500
mm
Standard Length
3 - 6
m
Custom Length
Cut to length on request
-
Diameter Tolerance
Per ASTM A29 / A29M for hot-rolled bar or as agreed for forged rounds
-
Length Tolerance
Per ASTM A29 / A29M or as agreed
-
Straightness Tolerance
Per ASTM A29 / A29M or as agreed
-
End Condition
Square cut, saw cut, chamfered or as ordered
-
Surface Finish
As-forged and descaled, hot-rolled black, peeled, rough turned, machined
-
Cut-to-Length Availability
Available
-
Dimensional Standard
ASTM A29 / A29M for bar, ASME B16.5 and B16.34 for finished components
-

Dimensions & Sizes
Explore available diameters, lengths, and dimensional requirements for AS F92 Round Bar
Pricing for Alloy Steel F92 Round Bar
Round Bar Prices are generally quoted per kilograms or meters tonnes and can fluctuate with the global raw material and market prices. The final price will depend on a variety of factors, including the grade size, diameter, length, surface finish, the quantity and whether the bars are cut to length or in standard lengths.
For smaller quantities, we can also quote per metre or per piece basis once the required dimensions have been confirmed. Container-loads or orders that are larger in size are typically priced per tonne, based upon the specifications required and the supply conditions.
Please provide your desired dimensions, grades, length number, and end for a current quote including the lead time applicable and details for certification.

Pricing
Get current Alloy Steel F92 Round Bar pricing based on size, quantity, grade, finish, and delivery requirements.
Why Choose Us
Euro Steel Bars is an international distributor, stockist and exporter of stainless round steel bars that cover carbon, stainless alloy, special grades. We stock a variety of sizes and grades. We guarantee every order with mill test certificates as well as full quality-assurance documentation. Our name speaks to our roots: European-sourced materials that is backed by the certificates and rigor that buyers from Asia as well as the Gulf and Africa are looking for.
Each bar we deliver is accompanied by EN 10204 3.1 mill test certificates as well as complete documentation of quality, so what you receive corresponds to what’s written in the documents. We carry a selection of sizes and grades ready for transport, and cut length upon the request of customers, which results in quicker lead times, whether you’re ordering just a one-off spec or a complete project tonnage.
We operate an actual wholesale business that is that is supported with an internationally-operated supply chain therefore we are able to serve fabricators sourcing one grade the same way in the same way as an EPC contractor who is placing a large order. Our clients include manufacturers, fabricators EPC construction companies, engineers oil and gas projects as well as construction companies. we design our inventory as well as documentation to show what buyers need to bring projects forward.
Our customers trust us across Qatar, Oman, Bahrain, Kuwait, Jordan, Malaysia, Singapore, Thailand, Taiwan, Turkey, Italy and South Africa. If you’re looking to source an Gulf energy project, or a construction project within Southeast Asia, you get the same quality of certified material, the exact documentation, and the exact delivery procedure.
Frequently Asked Questions
What is Alloy Steel F92 Round Bar?
What standard does Alloy Steel F92 Round Bar comply with?
What is the difference between F91 and F92?
What heat treatment is required for F92?
What are the key mechanical properties of F92?
Why is welding F92 so tightly controlled?
What is the service temperature range for F92?
What sizes are available in F92 round bar?
Request A Quote
Need a specific grade, size or quantity? Get pricing and availability for your requirement.